새 탭에서 열립니다
혁신적인 공기질 솔루션
COMPLIANCE ENGINEERING SUPPORT

Product Certification & Compliance Support
Integrate safety, EMC, wireless, ozone, performance, materials, labeling, and market-specific compliance requirements into product development before tooling and mass production.
Safety Compliance
EMC & Wireless
Pre-Compliance Testing
Multi-Market Planning
Discuss Your Compliance ProjectExplore Our Compliance Process
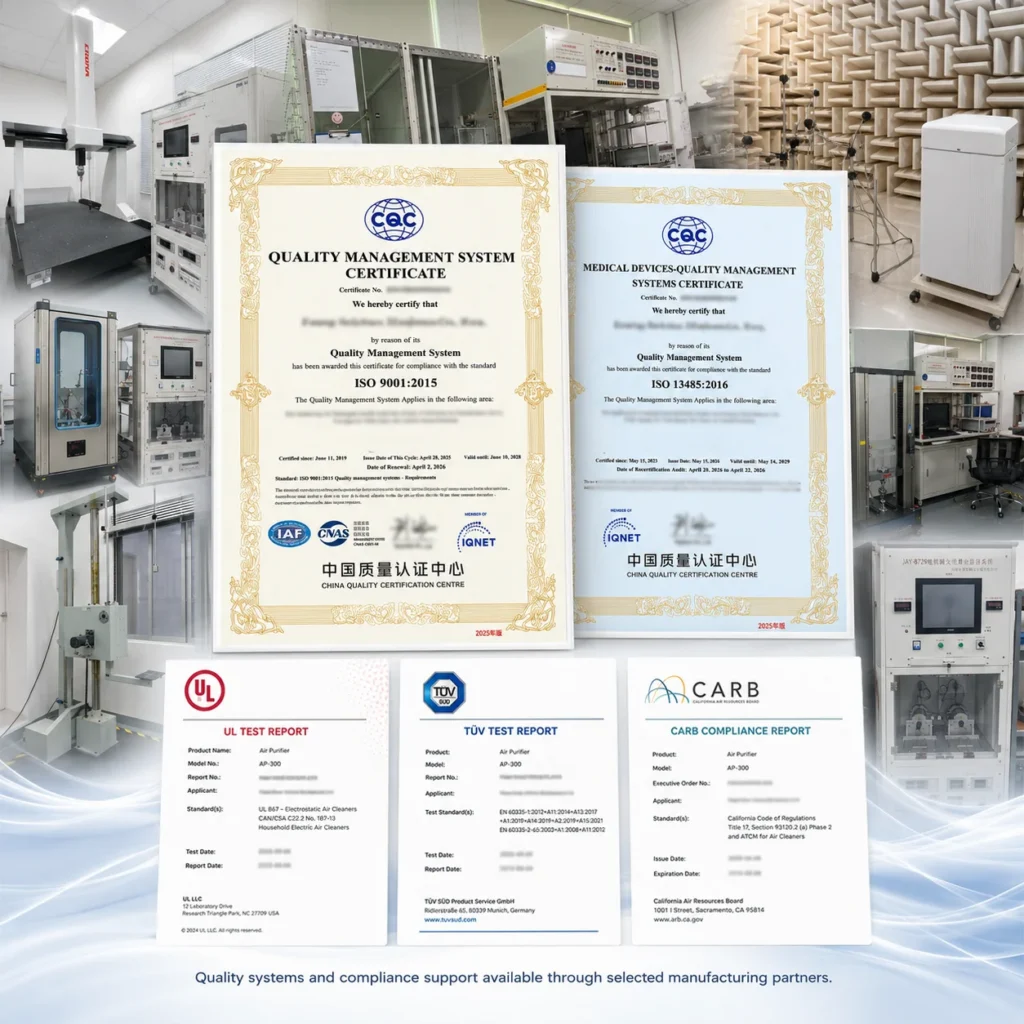
Certificates for quality management systems and test reports displayed alongside manufacturing and testing equipment.
COMPLIANCE AREASSafety / EMC / Wireless / Ozone
MARKETSNorth America / EU / UK
ENGINEERINGDesign / Pre-Test / Rectification
DOCUMENTATIONBOM / Labels / Manuals / Technical Files

How Our Compliance Support Works

Translate market and regulatory requirements into practical engineering, testing, documentation, and certification-coordination actions before product launch.
Market & Standards Planning

Define target markets, applicable certification scope, required samples, project responsibilities, and certification timing.

→
Design for Compliance

Review electrical architecture, grounding, insulation, temperature rise, critical components, materials, wireless functions, labels, and manuals before design freeze.

→
Pre-Compliance Testing

Perform relevant safety, EMC, wireless, temperature-rise, ozone, and performance pre-checks before formal third-party testing.

→
Laboratory & Documentation Coordination

Prepare samples, BOMs, critical-component lists, drawings, labels, and manuals, then coordinate technical questions and corrective actions with qualified third-party laboratories and certification bodies.

→
Compliance Planning
Design for Compliance
Pre-Compliance Testing
Lab & Documentation
Pre-Compliance Testing

Market & Certification Planning

Certification requirements vary by product category, electrical architecture, connectivity, purification technology, and target market. HisoAir develops a project-specific compliance roadmap before tooling and formal testing.
PROJECT DEFINITION

Target market definition
Applicable standards and certification scope
Product-category assessment
Sample requirements
Project responsibilities
Certification timeline planning

COMPLIANCE SCOPE

Electrical safety
EMC requirements
Wireless compliance
Ozone requirements
에너지 효율성
Product performance
Materials and labeling
Market-specific requirements

EVIDENCEAnechoic Chamber Data
Pre-Compliance Testing

Compliance Requirements Built into Product Design

Review structural, electrical, component, material, firmware, labeling, and documentation requirements before design freeze to reduce late-stage certification risks.
ENGINEERING REVIEW

Electrical architecture
Grounding and insulation
Temperature-rise risks
Abnormal operation considerations
Critical-component selection
Material requirements
Wireless functions
Structural compliance risks

DOCUMENT CONTROL

Critical-component lists
Controlled BOM
Rating labels
User manuals
Technical drawings
Material specifications
Firmware configuration
Market-specific documentation

EVIDENCEAnechoic Chamber Data
Pre-Compliance Testing

Pre-Compliance Testing Before Formal Certification

Perform relevant engineering pre-checks before formal third-party testing to identify compliance risks earlier and reduce avoidable test failures and redesign.
PRE-CHECK AREAS

Electrical safety
Temperature rise
Abnormal operation
EMC
Wireless functions
오존
Product performance
Applicable functional checks

ENGINEERING ACTIONS

Risk identification
Prototype evaluation
Test-condition review
Measurement verification
Structural correction
Electrical correction
Material correction
Firmware correction
Retest preparation

EVIDENCEAnechoic Chamber Data
Pre-Compliance Testing

Laboratory & Certification Documentation Coordination

Prepare certification samples and controlled technical documentation, then coordinate technical questions, corrective actions, and project execution with qualified third-party laboratories and certification bodies.
DOCUMENTATION SUPPORT

Certification samples
Controlled BOMs
Critical-component lists
Technical drawings
Rating labels
User manuals
Supporting technical files
Configuration records

PROJECT COORDINATION

Laboratory communication
Technical question follow-up
Corrective-action coordination
Sample preparation
Document revision
Retest coordination
Certification-status tracking
Production configuration alignment

EVIDENCEAnechoic Chamber Data

Real Compliance Engineering Evidence

Engineering, testing, documentation, and production-control records showing how compliance requirements are translated into real product-development actions.

Anechoic Chamber Testing
PLANNING

Certification Matrix

Project-specific certification planning defining target markets, applicable requirements, samples, responsibilities, and timing.

Evidence:Market / Standards / Scope
Anechoic Chamber Testing
SAFETY

Electrical Safety & Temperature Testing

Engineering pre-checks for electrical safety, temperature rise, abnormal operation, and related product risks.

Safety / Temperature
Anechoic Chamber Testing
EMC / WIRELESS

EMC & Wireless Pre-Compliance

Pre-compliance evaluation of EMC and wireless functions before formal third-party testing.
EMC / RF
Anechoic Chamber Testing
DOCUMENTATION

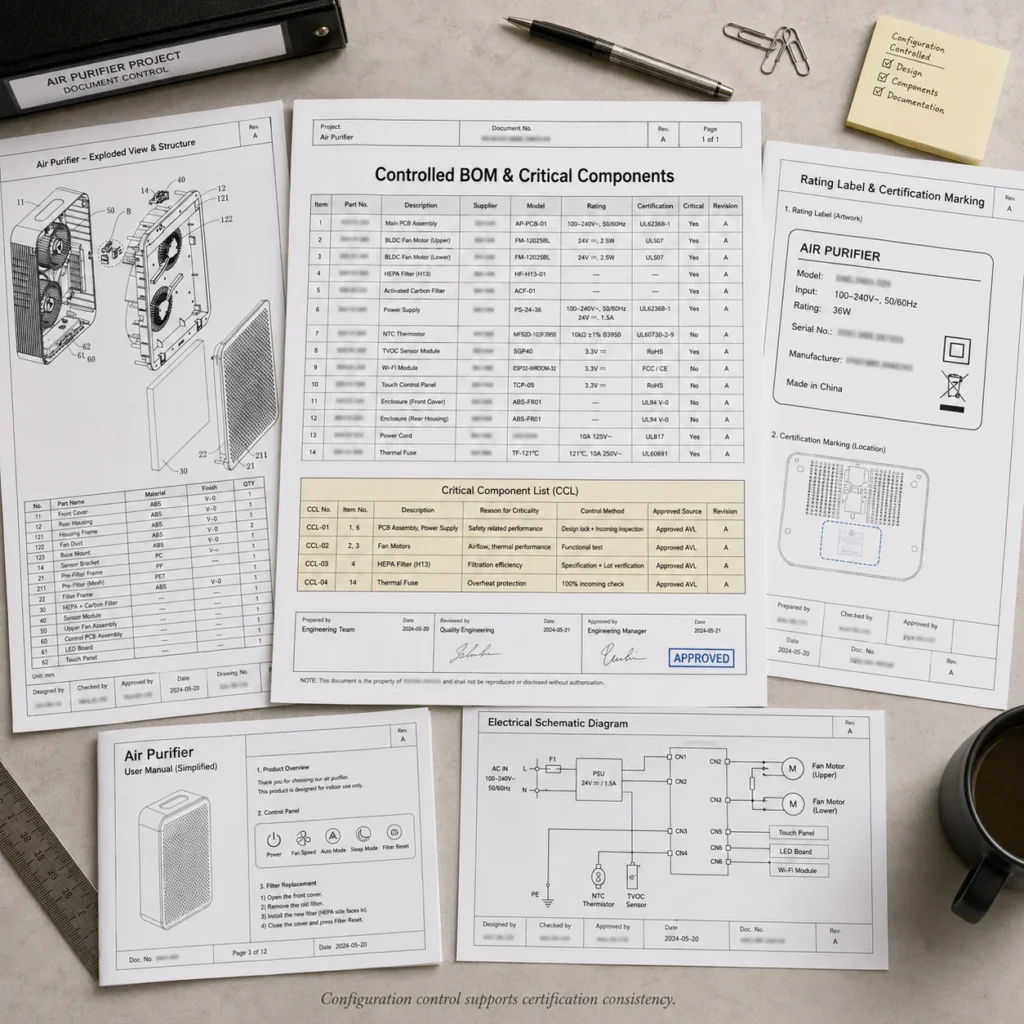
Controlled BOM & Critical Components

BOMs, critical-component lists, drawings, rating labels, and manuals maintained for certification and configuration control.

BOM / CCL / Documents
Anechoic Chamber Testing
RECTIFICATION

Compliance Corrective Engineering

Structural, electrical, material, or firmware modifications used to address compliance risks identified during engineering review or testing.
Design / Electrical / Firmware
Anechoic Chamber Testing
PRODUCTION CONTROL

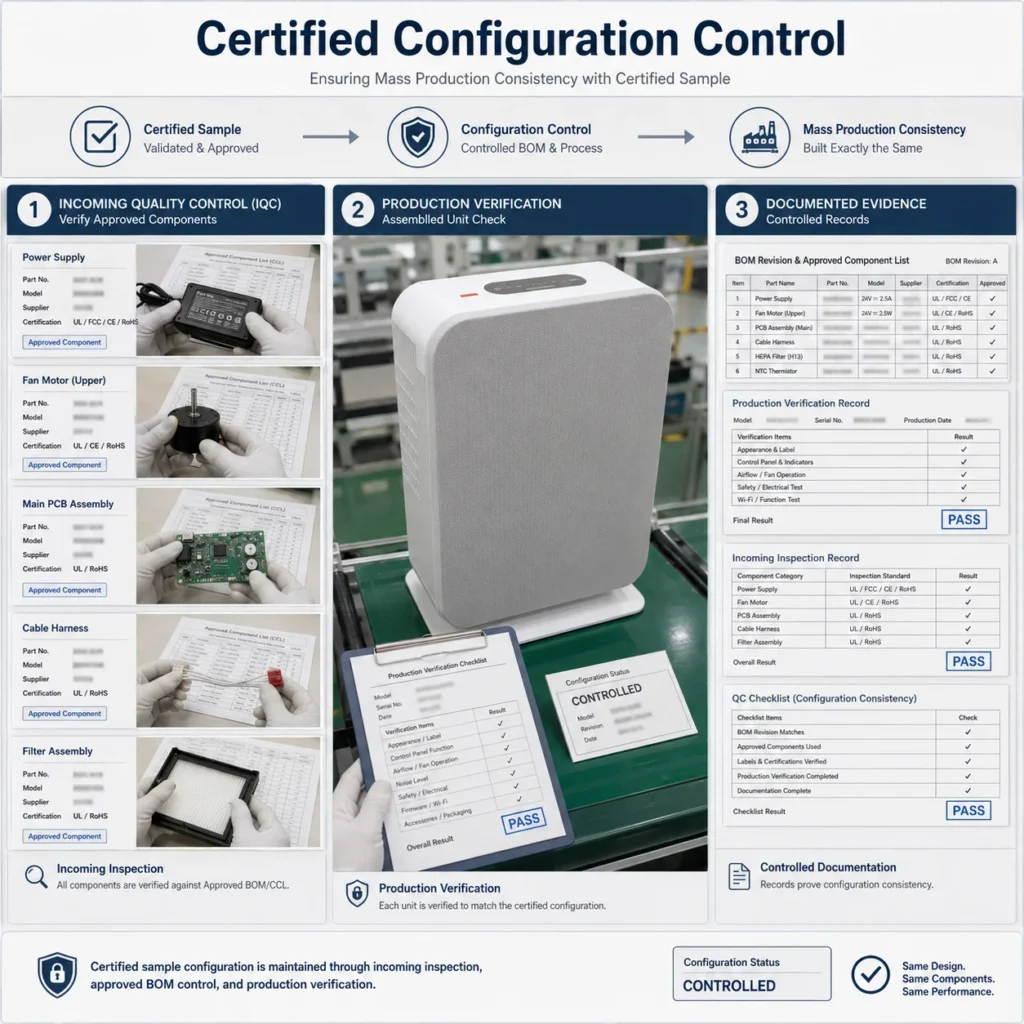
Certified Configuration Control

Certified BOM management, supplier-change assessment, incoming-component verification, and production-conformity control.

BOM / Supplier / Production

From Compliance Planning to Certified Production

Separate internal engineering validation from formal third-party certification and maintain the approved product configuration through production.

Compliance-Ready Design

Integrate applicable compliance requirements into product architecture, components, materials, firmware, labels, and documentation before tooling.

Pre-Compliance Validation

Perform engineering pre-checks and corrective actions before submitting the product for formal third-party testing.

Third-Party Certification

Submit controlled samples and documentation to qualified laboratories and certification bodies for applicable formal testing and certification.

Production Conformity

Maintain the approved BOM, critical components, materials, firmware, documentation, and production controls after certification.

Project Evidence

Real engineering cases where our compliance expertise accelerated market entry.
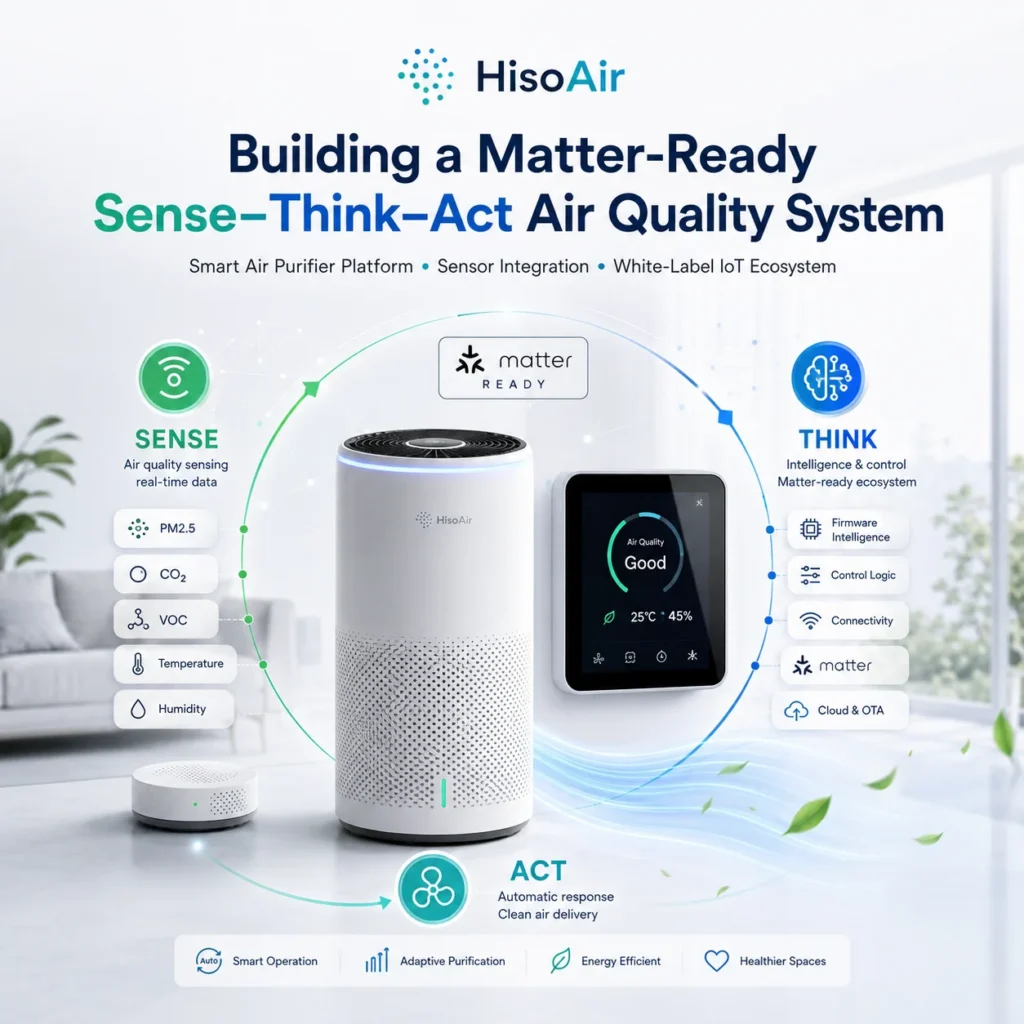
Matter over Thread Air Purifier
IoT Air Quality System / Smart Building Environmental Control(Germany / Europe)

Smart Air Quality System

CHALLENGE

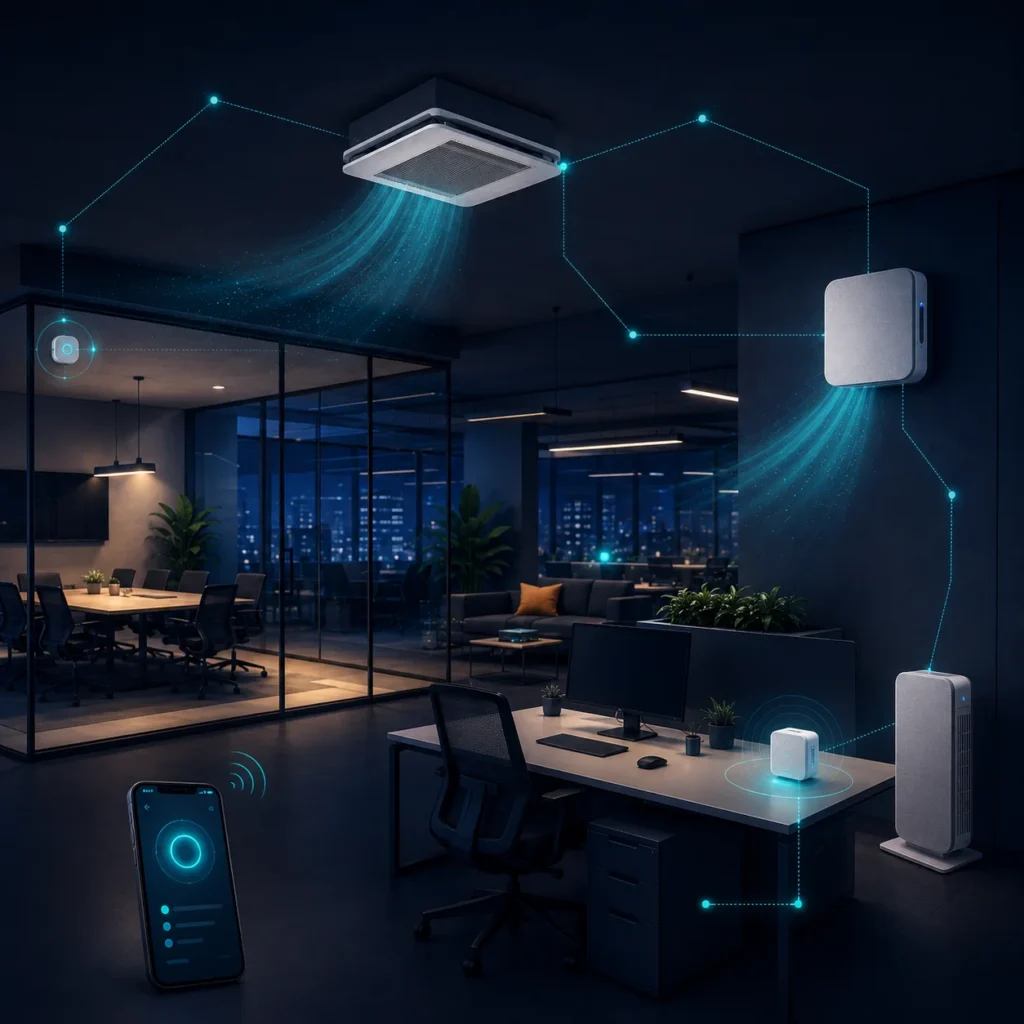
The client needed more than a standalone air purifier. The challenge was to integrate purification hardware with its own smart panel, sensors, firmware, control logic, and IoT ecosystem while evaluating Matter compatibility and maintaining the flexibility required for white-label product development.

ENGINEERING WORK

HisoAir provided Matter-ready air purifier platforms, sensor integration, firmware adaptation, and white-label support built around a Sense–Think–Act architecture—connecting environmental sensing, intelligent control logic, purification hardware, and the client’s own smart home or building ecosystem.

Result:

The initial evaluation established HisoAir as a potential system-level partner for the client’s connected air quality ecosystem, creating a roadmap for Matter integration, firmware adaptation, white-label products, and future Sense–Think–Act indoor environmental control solutions.
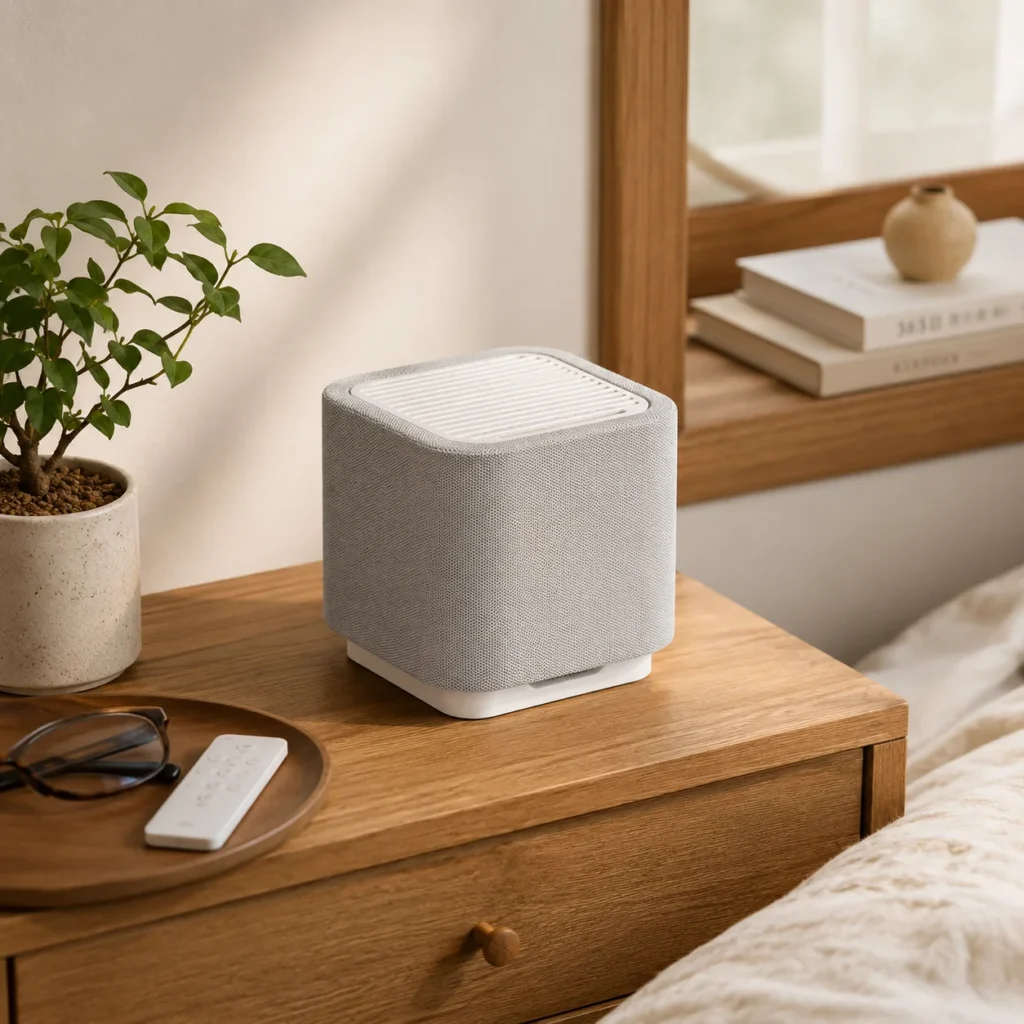
Matter over Thread Air Purifier
Smart Air Purification / Healthcare Consumer Electronics(Japan)

Smart Air Purification

CHALLENGE

Entering air purification was a new challenge for the client, requiring expertise beyond traditional consumer electronics. The product needed to be compact, quiet, and suitable for Japanese homes while delivering meaningful differentiation through smart connectivity—without the cost and complexity of building a proprietary app and cloud platform.

ENGINEERING WORK

HisoAir provided a proven compact desktop air purifier platform and integrated Matter over Thread connectivity, enabling compatibility with major smart home ecosystems. The platform also created a future-ready path toward Air+ IAQ / IEQ sensing and broader connected healthy-environment applications.

Result:

The client gained a differentiated and faster entry into Japan’s air purification market with a product aligned with its consumer electronics DNA. Matter over Thread reduced the need for independent app development while establishing a scalable foundation for future sensor-driven products and smart indoor environment solutions.
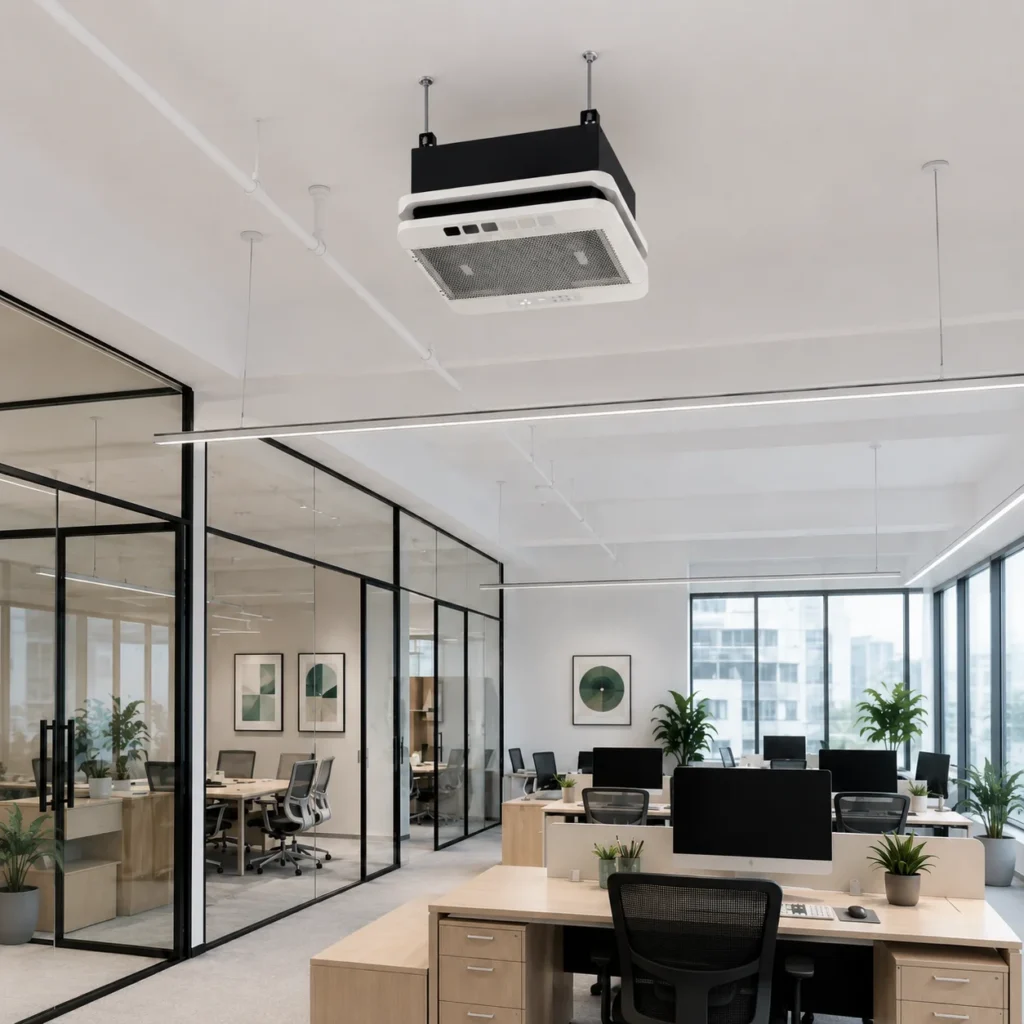
Matter over Thread Air Purifier
Healthy Building / Office Air Purification(Canada)

Healthy Building Air Purification

CHALLENGE

The client needed to improve air quality across different corporate office spaces while supporting workplace wellness and healthy-building objectives. The solution also needed to make environmental performance measurable through IAQ and IEQ data rather than relying on standalone purification devices alone.

ENGINEERING WORK

HisoAir combined ceiling-mounted and wall-mounted air purifiers with IAQ sensing for PM2.5, VOC, CO₂, temperature, and humidity, while extending the platform toward IEQ monitoring such as light, noise, occupancy, and people-counting for broader healthy-building applications.

Result:

The project created a cleaner, more measurable corporate workplace environment, with the client reporting improved comfort and significantly fewer sick-leave cases. It also established an IAQ and IEQ sensing foundation for future data-driven building management and intelligent environmental control.
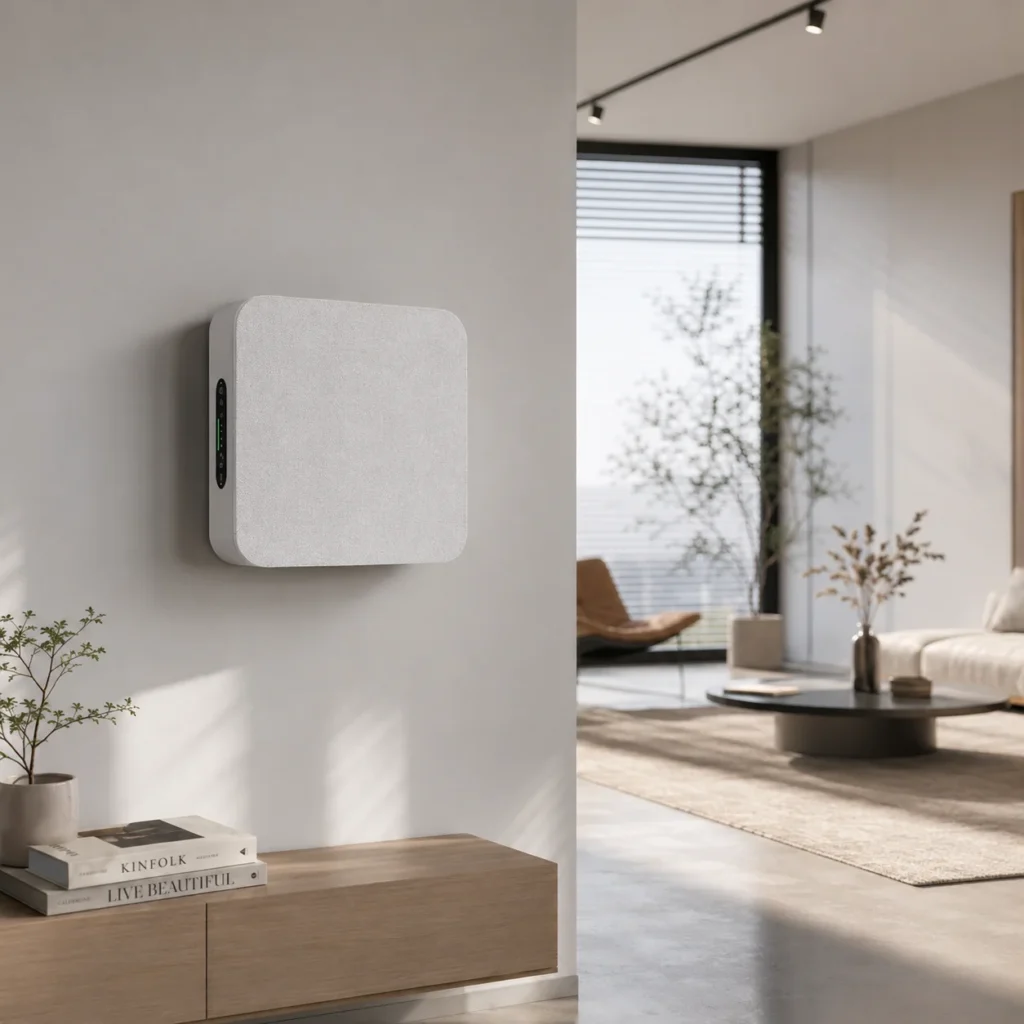
Matter over Thread Air Purifier
Allergy Care & Mold Resistance Air Purification(United States)

Wall Mounted Air Purification

CHALLENGE

The client needed to move beyond basic negative-ion products and develop a stronger purification platform capable of addressing allergy and mold concerns while meeting the continuous-operation, low-maintenance, and minimal-disturbance requirements of both residential and commercial environments.

ENGINEERING WORK

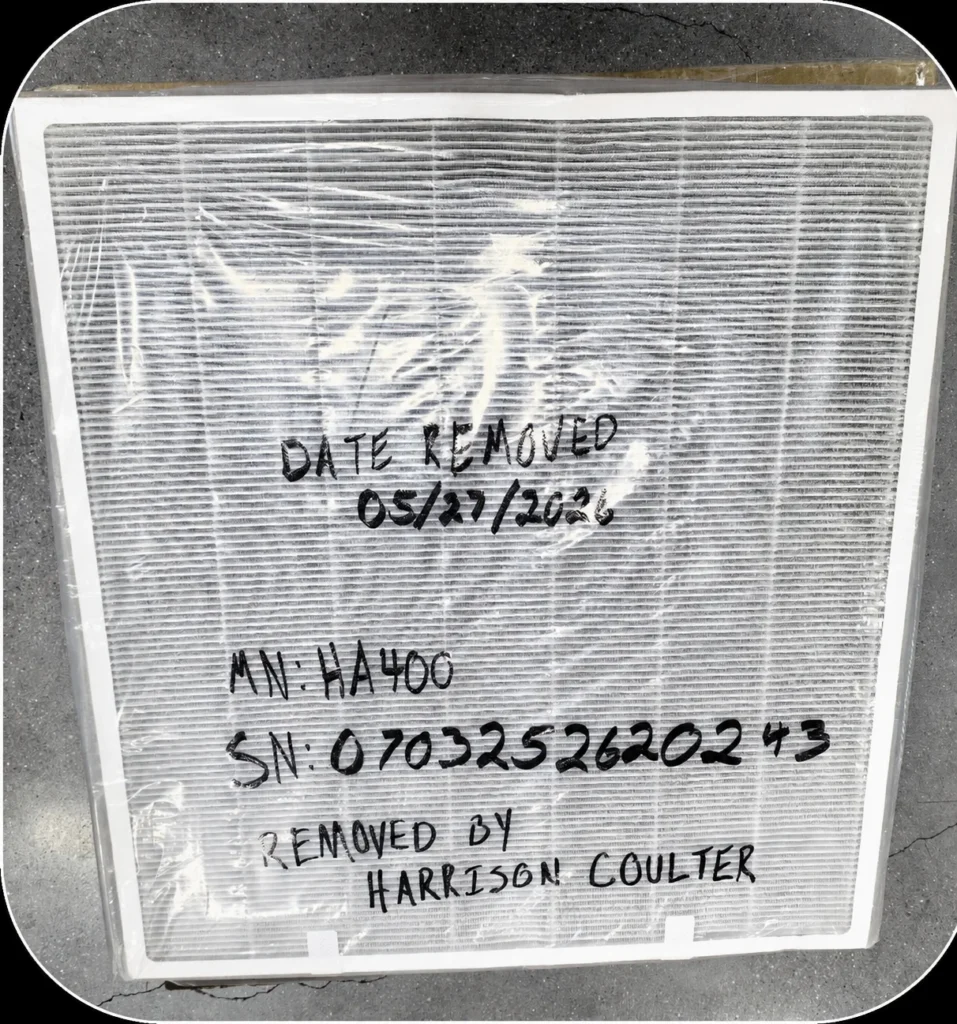
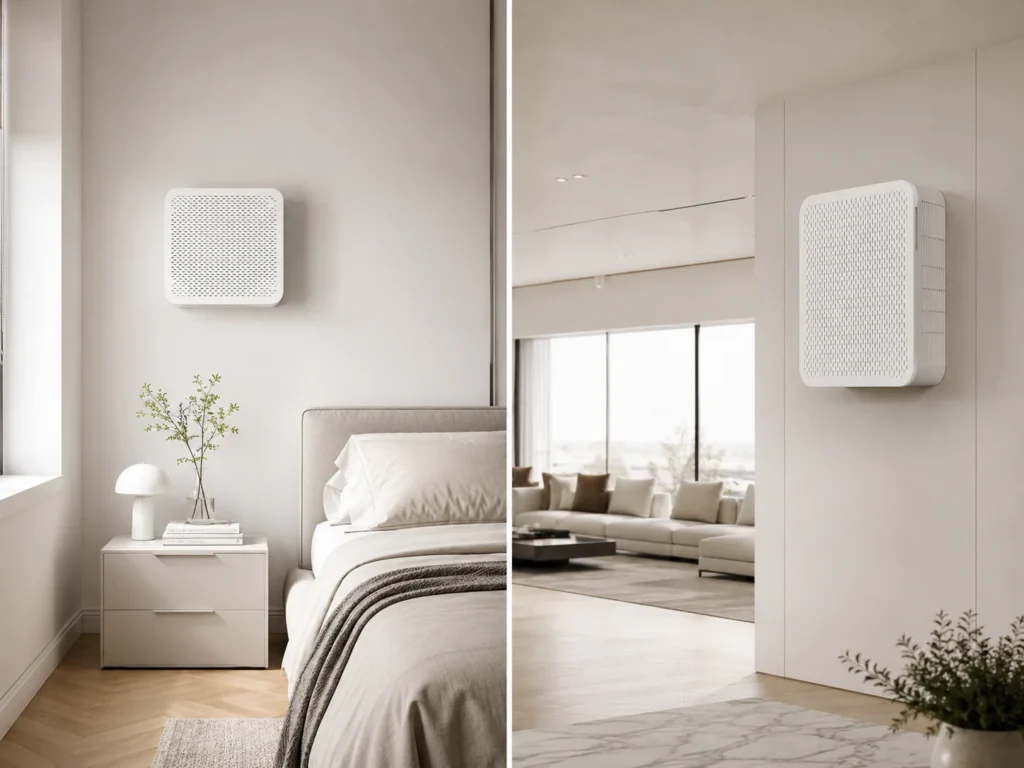
HisoAir introduced the proven HA200 and HA400 wall-mounted platforms with customized silver-ion filtration, long dust-holding capacity, smart auto mode, and a no-disturbance interface, creating a more professional and scalable solution for allergy and mold-related applications.

Result:

The client successfully upgraded from basic ionizer products to a differentiated wall-mounted purification portfolio with stronger filtration, mold-resistant filter customization, up to one-year filter life, and commercial-ready automatic operation for both residential and professional markets.

Ready to leverage our air treatment core
capabilities?

Partner with Hisoair for your next ODM project. Get access to our world
class manufacturing and R&D facilities.
Discuss Your Next Project
Contaminant Engineering•3 min read

PFAS Water Filtration Technologies Explained: Carbon, Resin & RO

Key Takeaway:

PFAS reduction depends on the specific compounds present, treatment media, contact time, water chemistry, and system design. Activated carbon, ion exchange, and Reverse Osmosis address PFAS through different mechanisms.

PFAS are a large family of persistent fluorinated compounds that can occur in drinking-water supplies. Their treatment behavior varies significantly by molecular structure, chain length, functional group, concentration, and the chemistry of the source water.

Granular Activated Carbon (GAC) removes PFAS primarily through adsorption. It is generally more effective for many longer-chain PFAS, while shorter-chain compounds tend to break through more quickly. Carbon performance depends on media properties, Empty Bed Contact Time (EBCT), competing organic matter, loading, and replacement frequency.

Ion-exchange resins use charged functional sites to capture many PFAS compounds. Properly selected anion-exchange media can provide high capacity and may perform better than conventional activated carbon for some shorter-chain PFAS, although performance still depends on water chemistry and competing ions.

Reverse Osmosis (RO) uses membrane separation rather than adsorption. Properly designed RO systems can provide broad reduction across many PFAS compounds as well as dissolved salts and other contaminants. Unlike carbon or resin, however, RO also produces a concentrate stream that must be managed.

No single technology should be selected from a PFAS label alone. System design should consider which PFAS compounds are present, their concentrations, required reduction targets, flow rate, media life, and the applicable third-party certification or validation requirements.

HisoAir Water Technical Series
Product Discovery•3 min read

How to Choose an Under-Sink Water Purifier for Modern Kitchens

Key Takeaway:

Match the treatment technology to your water quality first, then evaluate cabinet space, faucet configuration, flow rate, drain and power requirements, and filter replacement needs.

Choosing an under-sink water purifier starts with water chemistry. Carbon filtration is well suited to chlorine, taste, odor, and many organic contaminants, while Reverse Osmosis is more appropriate when dissolved salts, fluoride, nitrates, or broader dissolved contaminants need to be reduced.

For compact kitchens, tankless RO systems eliminate the conventional storage tank and can significantly reduce the space required under the sink. However, membrane capacity stated in GPD does not directly equal faucet flow. When comparing systems, check the actual dispensing flow rate, inlet-pressure requirement, recovery ratio, and whether a booster pump is required.

Installation architecture also matters. Many RO systems require a drain connection, electrical power, and either a dedicated drinking-water faucet or a compatible multi-function faucet. High-flow carbon systems can often connect directly to the existing cold-water line with a simpler installation, but pressure drop and available faucet flow should still be verified.

RO also removes much of the naturally occurring dissolved mineral content. Where taste or mineral balance is a priority, a post-RO remineralization stage can be added. Filter life should be evaluated by both rated capacity and local water quality rather than replacement time alone.

The right system is therefore not simply the smallest or highest-GPD model. It is the configuration that matches the target contaminants, available cabinet space, desired faucet setup, peak dispensing demand, and maintenance expectations.

HisoAir Water Technical Series
Water Quality•2 min read

What Does TDS Mean in Drinking Water? Measurement vs Contaminant Reality

Key Takeaway:

A TDS meter estimates the overall concentration of dissolved ionic substances from electrical conductivity. It cannot identify specific contaminants or determine whether water is chemically safe.

Total Dissolved Solids (TDS) refers to the combined concentration of dissolved substances in water. Most handheld TDS meters do not measure TDS directly. Instead, they measure electrical conductivity (EC) and convert that reading into an estimated parts-per-million (ppm) value.

This means a TDS reading can indicate how much dissolved ionic material is present, but not what that material actually is. Calcium, magnesium, sodium, nitrates, and other dissolved ions can all contribute to conductivity, yet a simple TDS meter cannot distinguish between them.

TDS meters are also not suitable for detecting trace contaminants such as PFAS, many VOCs, pesticides, pharmaceuticals, or disinfection byproducts. These substances may be present at concentrations far below the level needed to noticeably change electrical conductivity.

A low TDS reading therefore does not guarantee safe drinking water, and a higher TDS reading does not automatically indicate contamination. Water-treatment decisions should be based on laboratory testing for specific contaminants of concern rather than TDS alone.

HisoAir Water Technical Series
Technology Selection•2 min read

RO vs UF Water Filtration: Understanding Pore Sizes & Dissolved Minerals

Key Takeaway:

Ultrafiltration can reduce bacteria, turbidity, and suspended particles while retaining most naturally occurring dissolved minerals. Reverse Osmosis provides much broader reduction of dissolved salts and smaller contaminants.

Ultrafiltration (UF) typically uses hollow-fiber membranes with pore sizes in the approximate 0.01–0.1 micron range. These membranes physically retain turbidity, suspended solids, colloids, and many microorganisms while allowing dissolved minerals and salts to remain in the water.

Reverse Osmosis (RO) operates at a much finer separation level. Unlike UF, RO can substantially reduce dissolved ions such as sodium, calcium, fluoride, nitrates, and other contributors to total dissolved solids (TDS). This makes RO more suitable when dissolved-salt reduction is a primary treatment objective.

UF generally requires less system pressure and produces little or no continuous concentrate stream in many point-of-use configurations. RO typically requires greater pressure and produces a reject-water stream, but delivers broader contaminant reduction.

For water with acceptable TDS and mineral content, UF can be a simpler mineral-retaining treatment option. Where dissolved salts, fluoride, nitrates, or broader dissolved contaminants are a concern, RO is generally the more appropriate technology.

HisoAir Water Technical Series
Technology Selection•4 min read

Carbon Block vs Reverse Osmosis: Which Fits Your Need?

Key Takeaway:

Choose RO for dissolved inorganic salts and heavy metals; choose Carbon Block for chemical taste/odor, no wastewater, and high line-pressure flow.

Reverse Osmosis (RO) and Carbon Block filtration represent two fundamentally different treatment methods: membrane separation and adsorption. Understanding these differences helps determine which technology is better suited to a specific water-quality requirement.

Reverse Osmosis uses a semi-permeable membrane with pore sizes of approximately 0.0001 microns. It can significantly reduce dissolved inorganic contaminants such as TDS, fluoride, nitrates, and certain heavy metals. Because water must be forced through the membrane, RO systems require sufficient pressure or a booster pump and generate a concentrated wastewater stream.

Carbon Block filtration relies primarily on adsorption through compressed activated carbon, commonly with nominal pore sizes around 0.5–5 microns. It is highly effective for chlorine, chloramines, VOCs, taste, and odor, while allowing substantially higher direct-flow rates without producing wastewater.

From an operating perspective, Carbon Block systems are generally simpler, require less energy, and avoid the water loss associated with RO. RO involves higher system complexity and operating cost, but provides substantially broader reduction of dissolved contaminants that Carbon Block alone cannot address.

HisoAir Water Technical Series

견적 요청하기